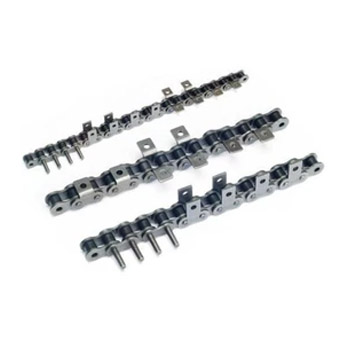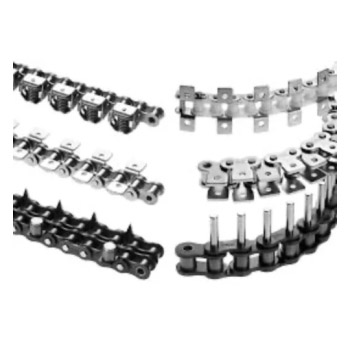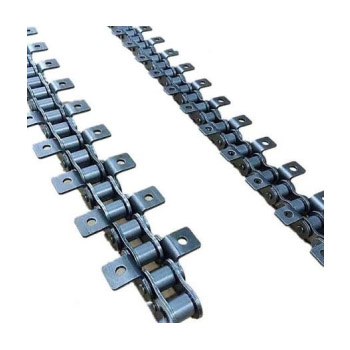
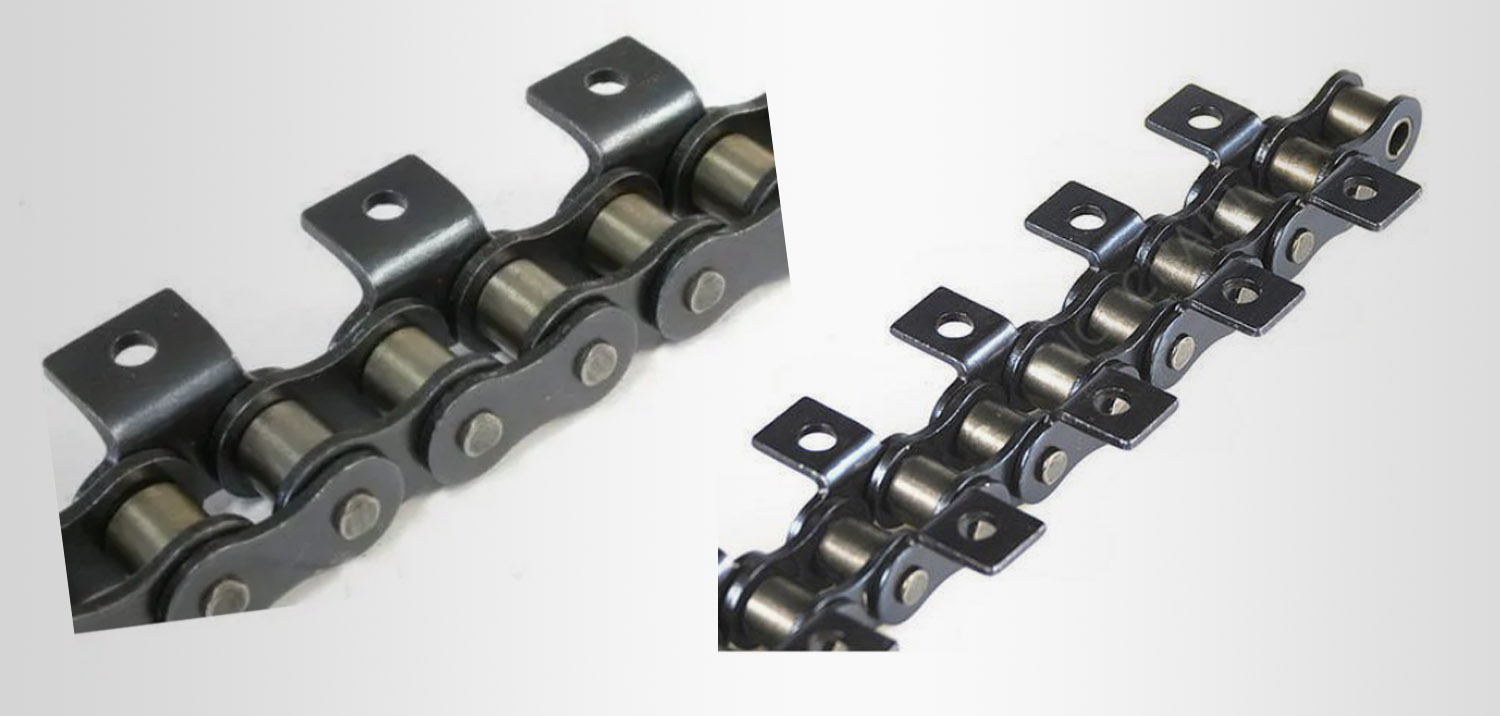
A conveyor chain is a specialized heavy-duty chain designed specifically for moving, transporting, or pulling materials along a production line or material handling system. Unlike standard power transmission chains (which are optimized to transfer rotational speed and torque between shafts), conveyor chains are engineered to carry loads directly—often featuring extended pins, rollers, or flat attachment plates to support items or interface smoothly with conveyor tracks.
Why Do We Use Conveyor Chains?
Conveyor chains are essential across manufacturing and industrial sectors for several key reasons :
- High Load Capacity : They can reliably support and transport extremely heavy raw materials, bulk goods, or finished products over long continuous runs without stretching or failing.
- Positive Drive (No Slippage) : Unlike flat rubber or fabric belts that rely on friction (and can slip under heavy loads), chain drives use rigid tooth-to-link meshing with sprockets, ensuring precise timing, synchronous movement, and zero slippage.
- Durability in Harsh Environments : Manufactured from hardened alloy steels, they withstand severe industrial conditions, including high temperatures, abrasive dust, moisture, and heavy shock loads.
- Versatility : By utilizing specialized attachments, flights, or extended pins, conveyor chains can be customized to push, pull, lift, or elevate materials horizontally, vertically, or around multi-planar paths.